ConveyorUP Solutions
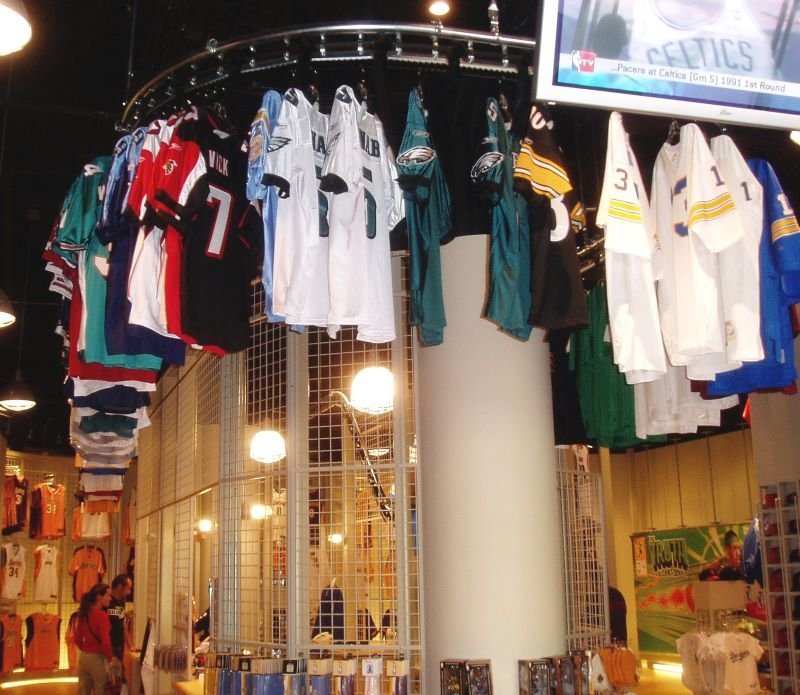
Retail Garment Display and Storage
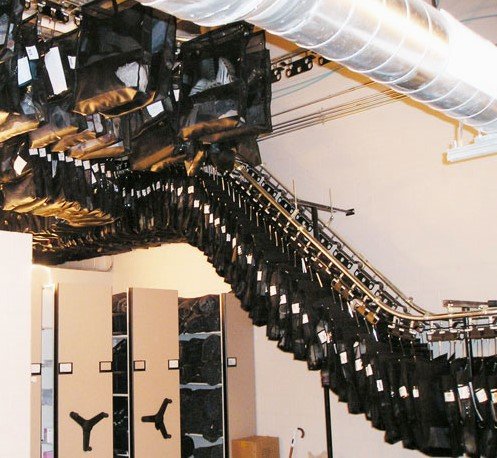
Property-bag Conveyor for Correctionals
Inmate property storage requires absolute reliability, security, and space efficiency. ConveyorUP’s automated property handling conveyors deliver a dependable, high-density storage and retrieval solution designed specifically for the demanding needs of correctional institutions.
- Maximize Available Space: Utilize unused overhead space to keep ground areas completely clear, or deploy multi-level configurations to double your storage capacity.
- Streamlined Operations: Speed up intake and release procedures with fast, automated garment and bag retrieval.
- Built for Continuous Duty: Constructed with industrial-grade components to guarantee maximum uptime, operator safety, and long-term durability
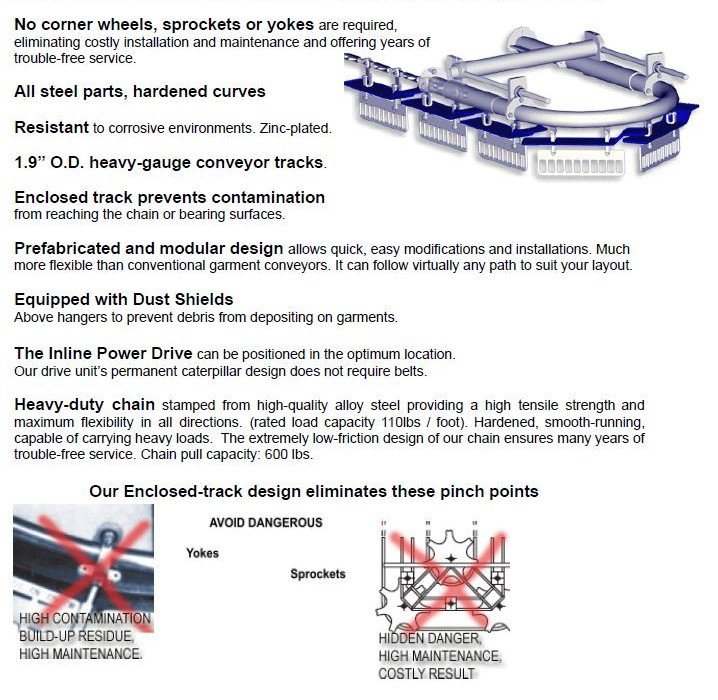
Benefits of Enclosed-Track Systems
Why chose ConveyorUP Systems?
ConveyorUP Systems specializes in custom overhead conveyor solutions for manufacturers, warehouses, distribution centers, finishing lines, and storage facilities
Operator Safety First
Fully enclosed track design eliminates exposed moving chain components, creating a safer work environment.
Flexible Layout Integration
Available with multiple curve radii and configurations to navigate tight spaces, complex layouts, and facility obstacles.
Compact & Modular Design
Space-saving overhead systems maximize floor area and can be expanded, modified, or reconfigured as operational needs evolve.
Quiet, Efficient Operation
Enclosed chain technology reduces noise levels while providing smooth, reliable product movement.
Built for Industrial Demands
Constructed with high-tensile, heat-treated, zinc-plated alloy steel chain for exceptional strength, wear resistance, and corrosion protection.
Low Maintenance, Long Service Life
Engineered with minimal friction and durable components to deliver years of dependable, cost-effective performance.
Custom Solutions for Every Application
Each system is tailored to your facility, product requirements, and workflow, ensuring optimal efficiency and productivity.
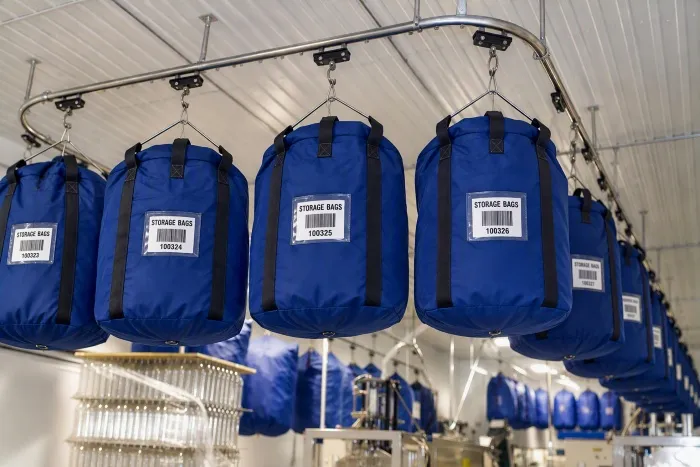
Oversize Storage Conveyor - Production Lines
Maximize Vertical Footprint: Elevate oversize bags into unused ceiling space to keep production aisles clear, safe, and open for machinery and foot traffic.
Automated Retrieval & Flow: Reduce manual handling and speed up inventory positioning directly to operational workstations.
Frequently Asked Questions
- Can the conveyor be expanded as our business grows?
Yes. Our modular design allows the system to be easily extended, shortened, or reconfigured as your operational needs change. - What is the typical lead time for delivery?
Standard delivery is 6-8 weeks. Depending on the system requirements and production schedule, some conveyors can be ready in as little as 1-3 weeks. - How does your pricing compare to other conveyor systems?
Despite being built with heavy-duty steel components for long-term durability, our conveyors are competitively priced and offer excellent value. - What conveyor speeds are available?
Our systems can operate from 0 to 72 feet per minute (FPM), depending on the application and system size. - What is the maximum load capacity?
Our standard recommendation is up to 100 lbs (45.5 kg) per foot. Higher capacities can be achieved using specialized carrier configurations. - How long do your conveyor systems last?
With proper maintenance, our conveyors can provide decades of reliable service. Some systems installed in 1969 are still operating today. - How much maintenance is required?
After initial setup and break-in adjustments, most systems require only annual or semi-annual maintenance, depending on usage. - Are there design limitations?
Very few. The modular construction allows conveyors to navigate around, over, or under obstacles and adapt to complex facility layouts.