Vertical Conveyor Rail Systems
ConveyorUP combines proven enclosed-track conveyor technology with custom engineering expertise to deliver reliable, efficient, and application-specific material handling solutions tailored to your operational requirements.
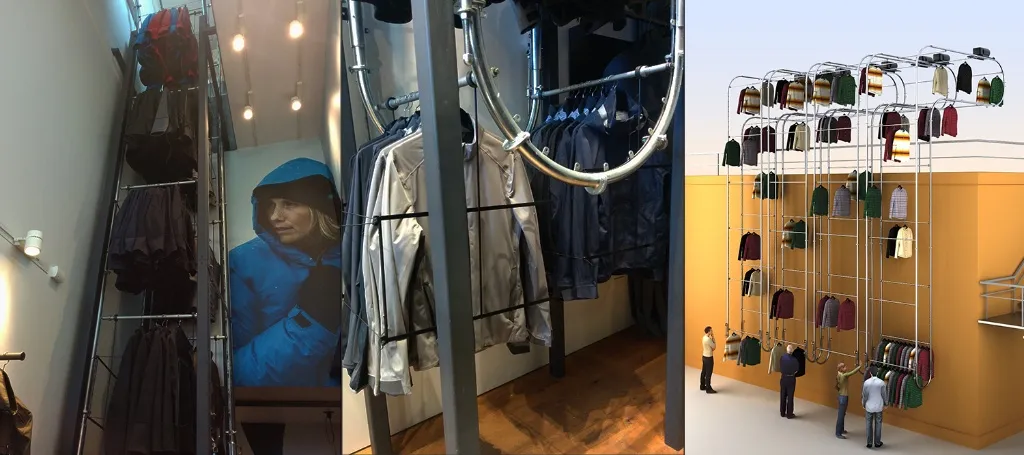
Vertical Conveyor System
Technical Specifications
- Load Capacity: 50 lbs per pendant
- Operating Speed: Up to 50 FPM
- Maximum Drive Pull: 600 lbs
- Chain Breaking Load: 3,700 lbs
- Chain Pendant Pitch: 6 inches
- Maximum Conveyor Length: 600 ft per drive (expandable)
- Standard Curve Radii: 9″, 12″, 18″, 24″, and larger
- Incline Capability: 30°, 45°, 60°, 90°, or custom angles
Benefits of Vertical Conveyor of Rail Storage Systems
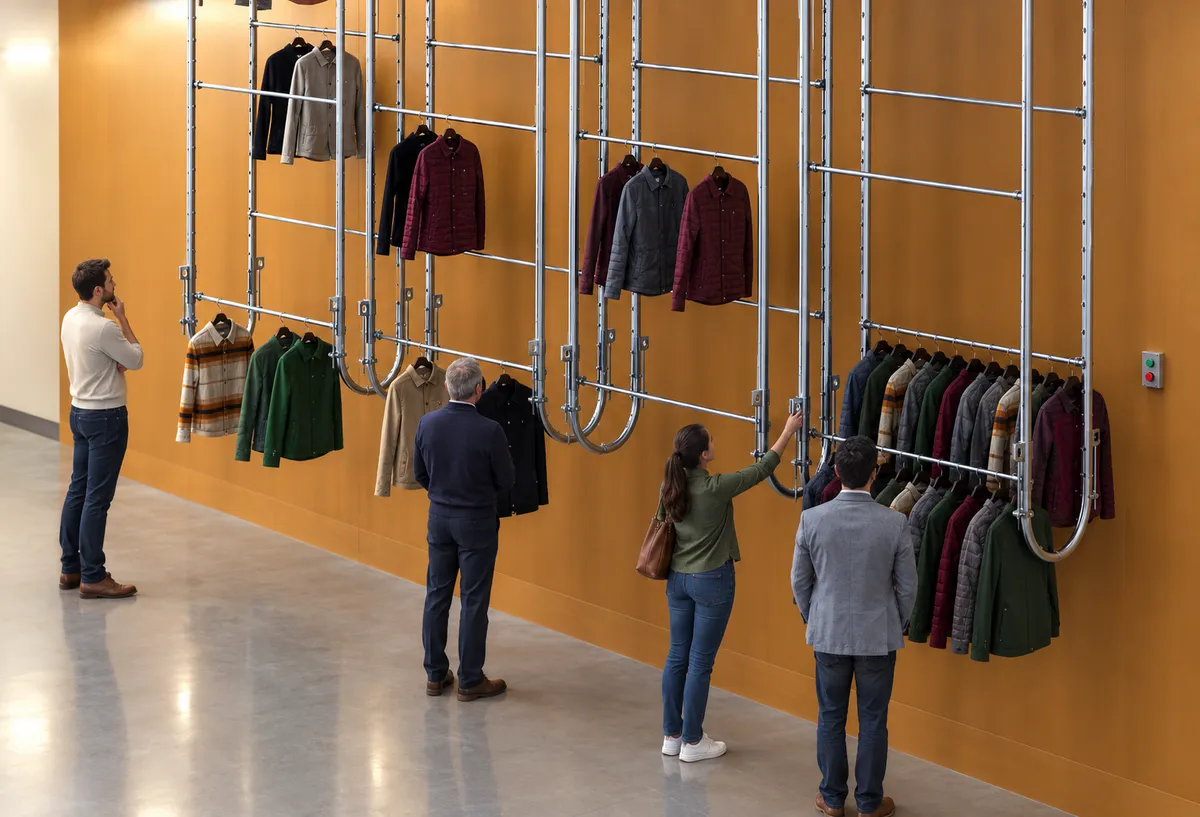
- Maximize Valuable Floor Space by utilizing unused overhead areas and freeing up production and work zones.
- Reduce Maintenance Costs with an enclosed-track design that protects chains and bearing surfaces from dust, debris, and contamination.
- Adapt to Any Facility Layout through a flexible modular design that allows for quick installation, easy expansion, and future system modifications.
- Ensure Reliable, Long-Term Performance with a heavy-duty chain and rugged all-steel construction engineered for demanding industrial environments.
- Resist Corrosion and Wear with durable components designed for dependable operation in challenging conditions.
- Maintain Cleaner Product Handling through enclosed-track construction that helps minimize exposure to contaminants.
- Enhance Workplace Safety by reducing exposed moving parts and pinch points commonly associated with traditional conveyor systems.
- Support Sustainable Operations by optimizing vertical space utilization and reducing facility footprint requirements.
- Quality and Reliability
- Supports Sustainable Operations
- Clean, Safe, Atractive
- Unique Space Saver
FAQ Frequently Asked Questions
What is a vertical conveyor rail system?
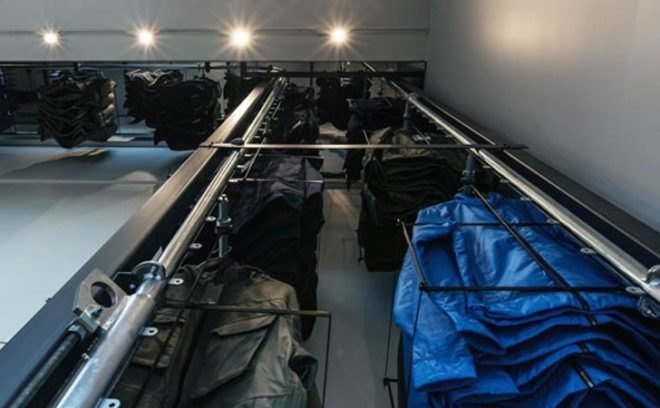
A vertical conveyor rail system transports products between elevations while utilizing overhead space to improve facility efficiency and reduce floor-space requirements.
What are the advantages of an enclosed-track conveyor?
Enclosed-track conveyors help reduce maintenance, protect components from contamination, improve safety, and provide long service life.
Can the system be customized?
Yes. ConveyorUP systems can be engineered to meet specific product, space, routing, and operational requirements.